Fabrication Station equipment
Bending machine.
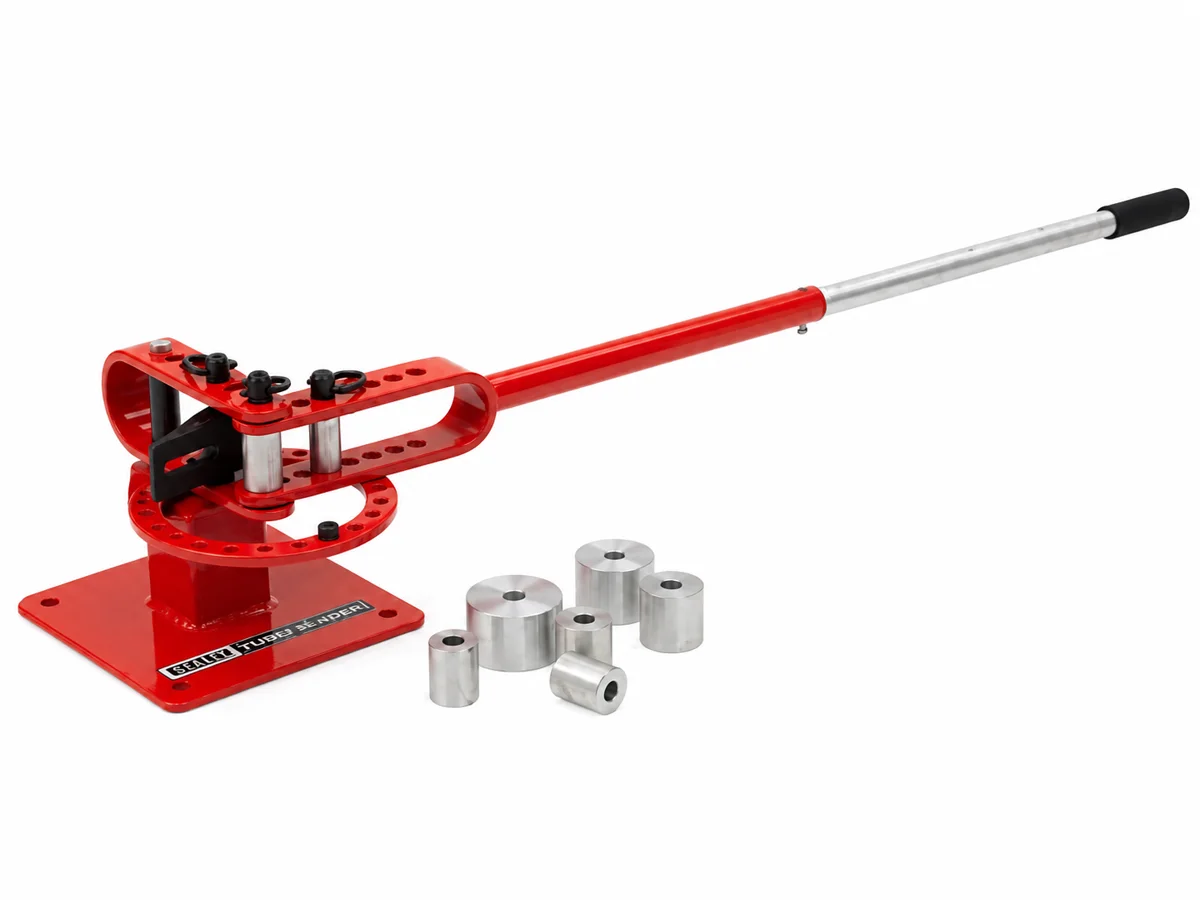
The workshop machine is a Clarke CCB1B compact parts bender. It forms bends in flat, square and solid round mild steel by pulling a hand lever around interchangeable dies.
Before you begin
- Complete the Fabrication Station bending-machine training before use.
- Check that the bender is secured to its bench or floor mounting.
- Wear safety goggles.
- Insert the hinge pins fully before making a bend.
- Leave enough material beyond the stop block and forming die that the work cannot pull free and release the handle suddenly.
- Bend hot-rolled mild steel only.
- Do not modify the bender or fit any handle extension other than the one supplied.
- Ask a technician about an unfamiliar setup. The Clarke operating instructions are kept at the station.
Material limits
| Material | Maximum |
|---|---|
| Flat stock | 5/16 × 2 in (about 8 × 50 mm) |
| Square or solid round stock | 5/8 in (about 16 mm) |
| Bending around the centre pin | 1/4 in (about 6 mm) thick; use the 1 in die for thicker stock |
| Sharp-angle-bend attachment | Flat stock only, 3/16 × 2 in (about 5 × 50 mm) or 1/4 × 1-1/4 in (about 6 × 32 mm) |
| Reinforcing bar | 1/2 in (about 13 mm) around the 3 in die only |
These are the limits published in the Clarke operating instructions. Metric values are approximate conversions. Never bend material other than hot-rolled mild steel, and never bend round stock with the sharp-angle-bend attachment.
Basic workflow
- Confirm the material and size are within the limits above.
- Fit the dies that give the radius you need, on the centre pin and in the handle.
- Select the handle hole and loop hole for the bend.
- Fit the stop block or the sharp-angle-bend attachment, with the block support underneath it.
- Position the stop block off-centre to the right and as close to the centre pin or die as the material allows.
- Insert the stock and set it for the first bend.
- Keep clear of the handle sweep and pull it through smoothly.
- Check the angle and position before making any further bends.
Revisit the demonstration

Load the parts bender video?
YouTube will receive information including your IP address when you load this video.
Watch on YouTube instead ↗Setting up and using a compact metal parts bender of this pattern. The video is not produced by the station, and the dies and attachments shown may differ from the ones held here.
Repeat bends and test pieces
- Make a test part from scrap of the same thickness before committing to final stock.
- For a series of identical parts, set the fixed stop in the next open hole, or use the adjustable stop when you need finer control, and tighten it before bending production parts.
- Write down the die sizes, hole positions and bending sequence so the setup can be repeated.
Common problems
The handle releases suddenly
There was not enough material beyond the stop block and die. Stop and start again with a longer blank.
The material slips or the stop block turns
The block is positioned off-centre to the left, or too far from the centre pin. Reposition it off-centre to the right and as close to the pin as the material allows.
The angle is not repeatable
Use the fixed or adjustable stop, and test on scrap of the same thickness before bending final parts.
The bend cracks
Check that the stock is hot-rolled mild steel, and move to a larger die so the bend radius is less severe.